The Role of Induction Hardening in Modern Metal Manufacturing
In modern metal manufacturing, components are expected to withstand high loads, repeated movement, friction, impact, and demanding operating conditions. Gears, shafts, crankshafts, camshafts, bearings, pins, and other metal parts must deliver reliable performance for long periods. Surface hardening is one of the most effective ways to improve their durability.
Among the available heat treatment technologies, induction hardening has become an important solution for manufacturers that need high precision, fast processing, and consistent results. The technology uses electromagnetic energy to heat selected areas of a metal component. The heated surface is then rapidly quenched to create a hard layer while the inner core remains relatively tough and ductile.
The role of induction hardening is therefore not limited to increasing surface hardness. It can improve wear resistance, fatigue performance, component life, and production efficiency. It can also help manufacturers treat specific areas of a component without exposing the entire part to high temperatures.
This makes induction hardening particularly useful in industries such as automotive, engineering, construction equipment, energy, and industrial machinery.
In this guide, we will examine how induction hardening works, why manufacturers use it, its major applications, important process parameters, advantages, limitations, and its growing importance in automated manufacturing.
What Is Induction Hardening?
Induction hardening is a surface heat treatment process used mainly for suitable grades of steel and other electrically conductive materials.
The process uses an induction coil to generate an alternating electromagnetic field. When a metal component is placed within this field, electrical currents are induced in the component. These currents generate heat directly inside the metal.
The surface is heated rapidly to a temperature suitable for austenitizing. Once the required temperature and depth are achieved, the heated area is cooled quickly using a suitable quenching medium.
This rapid cooling transforms the heated surface into a harder microstructure, typically martensite.
The result is a component with:
- A hard and wear-resistant surface
- A tougher internal core
- Improved resistance to fatigue
- Better resistance to repeated contact and friction
- Controlled treatment of selected areas
Unlike furnace-based processes, induction hardening can concentrate heat exactly where it is required.
Why Is Induction Hardening Important?
The main purpose of surface hardening is to provide a component with two different performance characteristics.
The outer surface needs to resist wear, contact stress, and fatigue. At the same time, the internal material needs enough toughness to absorb shock and mechanical loads.
Induction hardening can provide this combination.
For example, consider an automotive gear. The teeth experience repeated contact with another gear. If the surface is too soft, it can wear quickly. If the entire component is made extremely hard, however, it may become more susceptible to cracking or impact damage.
A controlled hardened layer provides a practical balance.
This is one of the key reasons the technology has become important in high-performance manufacturing.
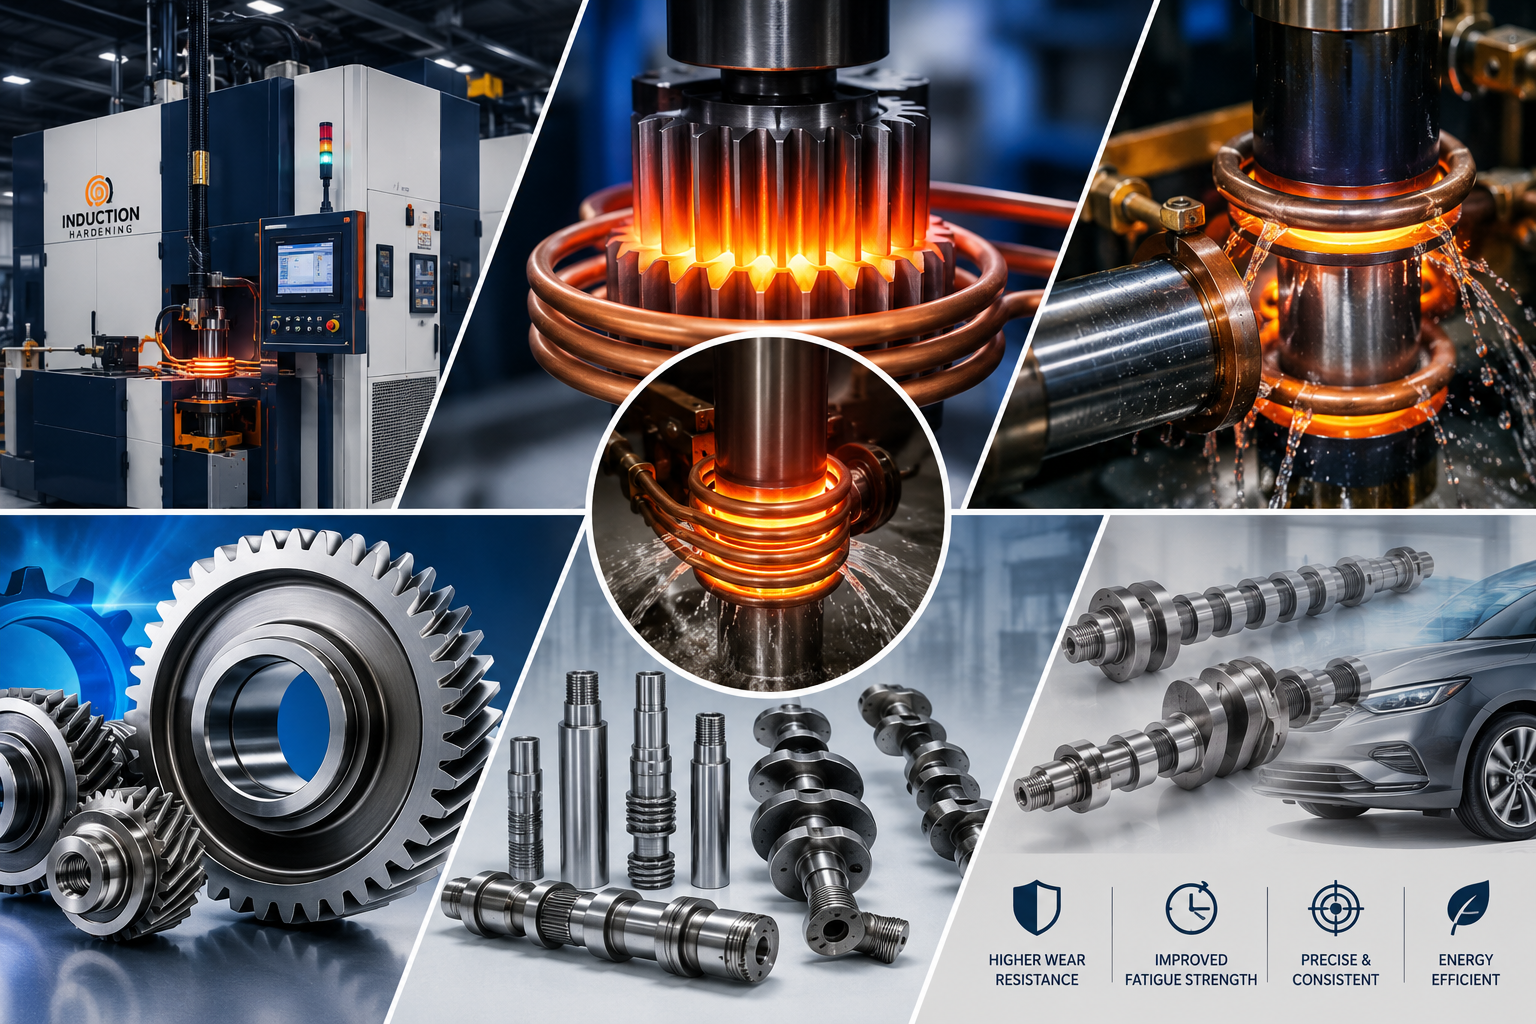
Key Benefits of Induction Hardening
1. Higher Wear Resistance
Metal components often operate under continuous friction and contact.
Gears, shafts, rollers, pins, and cams are exposed to surface wear throughout their service life. A hardened surface can withstand these conditions better than untreated material.
This helps reduce:
- Surface deformation
- Abrasive wear
- Adhesive wear
- Pitting
- Premature component replacement
For components that operate continuously, improved wear resistance can translate into lower maintenance requirements.
2. Improved Fatigue Performance
Repeated mechanical loading can cause small cracks to form at the surface of a component.
Over time, these cracks can grow and eventually lead to component failure.
A properly designed induction hardening process can create favorable compressive residual stresses near the surface. These stresses can make crack initiation and propagation more difficult.
This is particularly valuable for parts subjected to:
- Repeated bending
- Rotational loads
- Torsion
- Contact stress
- Cyclic loading
For automotive and industrial components, improved fatigue performance can significantly influence service life.
3. Tough Core and Hard Surface
One of the biggest advantages of the process is the ability to harden only the required region.
The surface receives intense heating, while the core is exposed to considerably less thermal influence.
This allows manufacturers to achieve a useful combination of:
Hard surface + tough core
The surface provides wear resistance, while the core provides strength and impact resistance.
4. Fast Processing
Induction heating can reach the required temperature much faster than many conventional heating methods.
The heating cycle can often be completed in seconds, depending on:
- Material
- Component geometry
- Required hardening depth
- Frequency
- Power
- Coil design
Shorter cycle times can increase production capacity, particularly in high-volume manufacturing.
5. Precise Heating
The heating area can be carefully controlled using the correct coil design and process parameters.
This is useful when only a specific section of a component requires hardening.
For example, a shaft may require hardening around a bearing seat while other sections remain untreated.
6. Repeatable Results
Modern induction hardening equipment can incorporate automated controls for power, frequency, heating time, temperature, scanning speed, and quenching.
This helps manufacturers maintain consistent processing conditions from one component to another.
Repeatability is especially important in automotive and mass-production environments.
How Does the Induction Hardening Process Work?
The process can be divided into several important stages.
1. Component Preparation
Before heating begins, the component should be clean and correctly positioned.
Oil, dirt, scale, and other contaminants can influence heating or quenching behavior.
The component geometry must also be considered because edges, holes, corners, and changes in section thickness can affect electromagnetic heating.
2. Positioning the Component
The component is placed in relation to the induction coil.
The distance between the coil and the workpiece, often referred to as the coil-to-workpiece gap, is an important process parameter.
Incorrect positioning can lead to uneven heating.
3. Electromagnetic Heating
Alternating electrical current flows through the induction coil.
This produces an alternating magnetic field around the coil. When the metal component enters this field, electrical currents are induced inside it.
The electrical resistance of the material converts these currents into heat.
Because the energy is generated within the component itself, induction heating can be extremely rapid.
4. Reaching the Required Temperature
The surface is heated to the required austenitizing temperature.
The exact temperature depends on the material grade and process requirements.
The heating must be controlled carefully.
Too little heat may result in insufficient transformation and inadequate hardness.
Excessive heating may lead to grain growth, distortion, surface damage, or other metallurgical problems.
5. Quenching
After heating, the component is rapidly cooled.
The quenching medium may include water, polymer solutions, oil, or other engineered fluids depending on the application.
The cooling rate must be controlled because it directly influences the resulting microstructure.
6. Inspection and Quality Control
After treatment, the component can be inspected for:
- Surface hardness
- Hardening depth
- Microstructure
- Distortion
- Cracks
- Dimensional accuracy
The inspection method depends on the component and customer specifications.
Important Parameters That Influence Results
Successful induction hardening requires more than simply heating a metal part.
Several parameters must work together.
Frequency
Frequency strongly influences the distribution of induced current within the component.
Higher frequencies generally concentrate heating closer to the surface.
Lower frequencies can allow deeper penetration of heating.
Therefore, frequency must be selected according to the required hardening depth and component geometry.
Power
Power determines how quickly the component can be heated.
The correct power level depends on factors such as component size, material, frequency, heating area, and cycle time.
Too much power can cause overheating.
Insufficient power can increase cycle time or prevent the component from reaching the required temperature.
Heating Time
Heating time affects both temperature and heat penetration.
A controlled heating cycle is essential for consistent results.
Coil Design
The induction coil is one of the most important elements of the system.
A properly designed coil can concentrate energy on the required region.
Coils can be designed for different component geometries, including:
- Gears
- Shafts
- Rings
- Bearings
- Crankshafts
- Camshafts
- Pins
- Custom components
Complex shapes may require specialized coil configurations.
Quenching Conditions
The quenching system must deliver consistent cooling.
Flow rate, temperature, concentration, pressure, and spray arrangement can all influence the final result.
Material Composition
Not every metal responds to induction hardening in the same way.
Steel grades with suitable carbon content and hardenability are commonly used.
The material’s chemical composition and previous heat treatment should be considered when developing a process.
Applications of Induction Hardening
The technology is used across several manufacturing sectors.
Automotive Components
The automotive industry is one of the major applications for induction hardening.
Components such as gears, shafts, crankshafts, camshafts, wheel hubs, steering components, and driveline parts can experience high mechanical loads.
Surface hardening helps these components withstand wear and cyclic stress.
For manufacturers looking specifically at automotive applications, the process can be integrated into automated production systems for high-volume component processing.
Gear Manufacturing
Gear teeth are exposed to repeated contact and sliding forces.
A properly hardened tooth surface can improve resistance to:
- Wear
- Pitting
- Contact fatigue
- Surface deformation
The ability to selectively harden the required regions makes induction technology particularly useful for gear production.
Shafts
Transmission shafts, drive shafts, axle shafts, and other rotating components can benefit from localized hardening.
Specific bearing seats, splines, shoulders, or other high-stress areas can be treated according to the component design.
Crankshafts and Camshafts
Crankshafts and camshafts experience repeated loading during engine operation.
Their journals, fillets, lobes, and other critical areas may require enhanced surface properties.
Induction hardening can provide localized treatment while maintaining the desired properties of the remaining material.
Heavy-Duty Equipment
Construction, mining, and agricultural equipment often operate under harsh conditions.
Pins, rollers, shafts, gears, and other components must withstand impact, abrasion, and continuous mechanical loading.
Surface hardening can extend the useful life of these parts.
Wind Energy
Wind turbine components operate under demanding and variable loads.
Large gears, shafts, and other drivetrain components require high fatigue resistance and durability.
Induction hardening can be used where localized surface treatment is suitable for the component design.
Induction Hardening Compared With Other Heat Treatment Methods
Manufacturers have several surface treatment options.
The correct choice depends on the material, component geometry, required hardness, production volume, depth, and cost.
Induction Hardening vs. Flame Hardening
Flame hardening uses a flame to heat the surface before quenching.
Induction heating, in contrast, uses electromagnetic energy.
Induction systems generally provide better control over heating location, cycle time, and automation.
Induction Hardening vs. Carburizing
Carburizing changes the surface chemistry by introducing carbon into the component during a controlled furnace process.
It can produce a deep hardened case but usually requires longer processing times.
Induction hardening primarily uses controlled heating and cooling without intentionally adding carbon to the surface.
This makes it attractive when localized hardening is required.
Induction Hardening vs. Conventional Furnace Heating
Furnace treatment heats the entire component or a large batch of components.
Induction heating can focus energy on selected areas.
This can reduce unnecessary heating and shorten processing cycles.
Challenges in Induction Hardening
Although the technology provides many benefits, successful implementation requires careful engineering.
Initial Investment
Induction equipment can require significant initial investment.
The system may include:
- Power supply
- Induction coil
- Heating station
- Quenching system
- Automation
- Control system
- Cooling equipment
However, production volume and long-term operating efficiency should be considered when evaluating the investment.
Coil Development
A poorly designed coil can produce uneven heating.
For complex components, coil development may require simulation, testing, and optimization.
Distortion
Rapid heating and cooling can create thermal stresses.
If the process is not correctly designed, dimensional changes may occur.
Process development should therefore consider component geometry, material properties, heating pattern, and quenching conditions.
Process Expertise
The equipment alone does not guarantee good results.
Experienced engineers must determine the correct combination of:
- Frequency
- Power
- Heating time
- Coil geometry
- Scanning speed
- Temperature
- Quenching conditions
Proper process development is essential.
Automation and Digitalization
Modern induction hardening systems are increasingly becoming part of automated manufacturing lines.
Automation can help control the complete cycle from component loading to inspection.
Sensors and control systems can monitor process conditions and identify deviations.
Modern systems may also incorporate:
- Automated component handling
- Recipe-based process control
- Temperature monitoring
- Quench monitoring
- Production data collection
- Machine diagnostics
- Quality traceability
This creates opportunities for manufacturers to improve both productivity and process consistency.
The Future of Induction Hardening
The future of induction hardening is closely connected with automation, digital manufacturing, energy efficiency, and advanced process control.
One important development is real-time monitoring.
Instead of relying only on post-process inspection, manufacturers can increasingly monitor process parameters during heating and quenching.
Artificial intelligence and data analytics may also help identify relationships between process parameters and final component quality.
Simulation technology can further support coil design and process development before physical production trials begin.
These developments can reduce development time and improve repeatability.
Another important trend is energy efficiency.
Because induction heating transfers energy directly to the component, it can be highly efficient for localized heating applications. Better power electronics and control systems are expected to improve this efficiency further.
How Manufacturers Can Choose the Right Induction Hardening Solution
Selecting an induction hardening system should begin with the component rather than the machine.
Manufacturers should define:
Component Material
Identify the exact material grade and its hardenability.
Required Hardness
Specify the target surface hardness and acceptable tolerance.
Hardening Depth
Determine how deep the hardened layer needs to extend.
Treatment Area
Identify the exact surfaces that require hardening.
Production Volume
High-volume production may require automated loading, unloading, scanning, and inspection.
Component Geometry
Complex geometries may require customized induction coils and specialized heating strategies.
Quality Requirements
Define dimensional, metallurgical, hardness, and inspection requirements before finalizing the process.
A complete evaluation of these factors helps ensure that the selected equipment can meet production objectives.
Why Induction Hardening Matters for Modern Manufacturing
Manufacturers today are under pressure to produce components that are stronger, lighter, more durable, and more economical.
At the same time, production systems must become faster and more energy efficient.
Induction hardening addresses many of these requirements through localized and controlled heating.
Its ability to harden selected areas without treating the entire component makes it particularly valuable for engineered parts.
The process can also be integrated with automated production systems, making it suitable for modern smart manufacturing environments.
For industries where component failure can result in costly downtime, improved surface durability can have a major economic impact.
Conclusion
The role of induction hardening in modern metal manufacturing goes far beyond simply increasing surface hardness. It provides manufacturers with a controlled method for improving wear resistance, fatigue performance, and service life while maintaining the toughness of the component core.
Its ability to deliver rapid, localized heating makes the technology suitable for a wide range of applications. Automotive gears, shafts, crankshafts, camshafts, industrial machinery components, and heavy-duty parts can all benefit when the process is correctly engineered.
The success of the treatment depends on several factors, including material composition, frequency, power, heating time, coil design, temperature, and quenching conditions. Proper process development is therefore essential.
As manufacturing moves toward greater automation and digital control, induction hardening is expected to become even more precise and efficient. Advanced monitoring, automated systems, improved coil designs, simulation, and data-driven process optimization will continue to expand its capabilities.
For manufacturers looking to increase component durability while maintaining production efficiency, induction hardening offers a powerful combination of precision, speed, repeatability, and localized surface treatment.